
 English
 Español
 Pусский
 Tiếng Việt
حزام ناقل مطاطي مقاوم للهب
Flame-Resistant Rubber Conveyor Belts: Features and Applications Flame-resistant rubber conveyor belts are specialized industrial belts designed to resist ignition, prevent flame propagation, and minimize the risk of fire in high-risk environments. These belts are essential in industries where combustible materials, high temperatures, or sparks are present, such as mining, power plants, chemical processing, and underground transportation. Key Features 1. Fire Resistance The primary characteristic of these belts is their ability to resist flames and self-extinguish when the ignition source is removed. They are manufactured using flame-retardant rubber compounds, often incorporating additives like antimony trioxide, chlorinated paraffins, or aluminum hydroxide to suppress combustion. 2. High-Temperature Stability Flame-resistant belts can withstand elevated temperatures without degrading. The rubber cover is formulated to resist heat aging, ensuring durability in hot environments such as steel mills or cement plants. 3. Anti-Static Properties Many flame-resistant belts also feature anti-static properties to prevent the buildup of static electricity, which could spark fires in volatile atmospheres (e.g., coal mines or grain handling facilities). 4. Durable Construction These belts typically consist of multiple layers, including a flame-resistant rubber cover, fabric or steel cord reinforcement, and a bottom cover. The reinforcement provides tensile strength, while the rubber layers ensure fire resistance and abrasion protection. 5. Compliance with Safety Standards High-quality flame-resistant belts meet international safety standards such as ISO 340, DIN 22103, and MSHA (Mine Safety and Health Administration) regulations. These certifications ensure the belts perform reliably in hazardous conditions. Applications - Mining Industry – Used in coal mines to transport materials safely, reducing the risk of fire from sparks or friction. - Power Plants – Ideal for conveying coal, ash, or other combustible materials near high-heat zones. - Chemical and Petrochemical Plants – Prevents fire hazards when handling flammable chemicals or oils. - Steel and Cement Industries – Withstands high temperatures and abrasive materials while maintaining fire safety. Advantages - Enhanced Safety – Reduces fire hazards, protecting workers and equipment. - Long Service Life – Resistant to heat, wear, and tearing, ensuring cost-effective operation. - Versatility – Suitable for various industries with demanding fire safety requirements. Conclusion Flame-resistant rubber conveyor belts are critical for industries where fire hazards are a concern. Their ability to resist ignition, self-extinguish, and operate under extreme conditions makes them indispensable for safe and efficient material handling. By selecting belts that comply with industry standards, businesses can ensure both operational reliability and workplace safety.
نتاج
تصنيف:
-
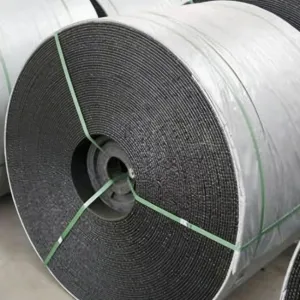
حزام ناقل مثبطات اللهب
تصنيفها: أنظمة الحزام الناقلالمشاهدات: 1364عدد:وقت الإصدار: 2025-12-28 18:28:04حزام ناقل مثبطات اللهبحل موثوق لحزام النقل الآمن ضد الحرائق للبيئات الصناعية عالية المخاطرنظرة عامة على المنتجأحزمة النقل المقاومة للهب عبارة عن أحزمة نقل مطاطية مصممة خصيصًا لمنع انتشار الحرائق وتقليل مخاطر الحرائق في البيئات الصناعية عالية المخاطر. في صناعات مثل التعدين، وتوليد الطاقة، وإنتاج الأسمنت، ومعالجة الصلب، ومناولة المواد السائبة، غالبًا ما تعمل أنظمة النقل في ظل ظروف وجود الحرارة أو الاحتكاك أو الشرر أو المواد القابلة للاحتراق. في ظل هذه الظروف، قد تشتعل سيور النقل العادية أو تسمح للهب بالانتشار بسرعة على طول خط النقل، مما يخلق مخاطر خطيرة على السلامة وخسائر محتملة في الإنتاج.تم تط...
أخبار
تصنيف:
-
[industry news]Seamless Endless Conveyor Belts for High Efficiency Producti...
2026-07-01 02:37:14 -
[industry news]TD75 Belt Conveyor Manufacturer for Bulk Material Handling
2026-07-31 02:33:17 -
[industry news]DY Mobile Conveyor Systems for Flexible Bulk Material Handli...
2026-08-15 02:17:40 -
[industry news]Portable DY Mobile Conveyor Belt Systems for Bulk Handling
2026-08-25 02:17:43 -
[industry news]TD75 Belt Conveyor Manufacturer with Custom Design Services
2026-09-15 15:23:53
حالة
تصنيف:
لا توجد نتائج بحث!
فيديو
تصنيف:
لا توجد نتائج بحث!
تحميل
تصنيف:
لا توجد نتائج بحث!
تجنيد
تصنيف:
لا توجد نتائج بحث!
المنتجات الموصى بها
-
NEWS
حزام ناقل مثبطات اللهب
مزيد من المعلومات



 واتس اب
 هاتف